High-Efficiency Transformer Assemblies & Cores
Explore our core product lines optimized for 22kV distribution systems, heavy metallurgical plant integration, and EU Ecodesign Directive Tier 2 compliance across Slovakia.
Metallurgical Precision & Magnetic Core Architecture for Slovak Utilities
A comprehensive analysis of loss reduction, domain refinement, and structural integrity in transformer core manufacturing for Central European electrical grids.
1. Cold-Rolled Grain-Oriented (CRGO) Steel vs. Amorphous Alloys: Core Material Selection
In modern power transmission and distribution, the magnetic core represents the heart of transformer efficiency. As Slovakia accelerates its transition toward smart grids under the European Union’s 2030 Climate Strategy, power grid operators like SEPS (Slovenská elektrizačná prenosová sústava) and regional distributors (ZSD, SSD, VSD) demand unprecedented reductions in no-load losses ($P_0$).
Our manufacturing facility leverages prime-grade Cold-Rolled Grain-Oriented (CRGO) silicon steel (ranging from conventional M0H, M1 grades to laser-domain-refined Hi-B steel 23ZDH085) and advanced Amorphous Ribbon Alloys (Metglas 2605SA1). The selection of core geometry and metallurgy directly governs the magnetostriction, eddy current dissipation, and overall lifecycle operating expenses (OPEX).
| Core Material Type | Nominal Thickness | Specific Core Loss (1.7T / 50Hz) | Saturating Magnetic Flux Density ($B_s$) | Slovakia Application Suitability |
|---|---|---|---|---|
| Domain Refined Hi-B CRGO | 0.23 mm - 0.27 mm | 0.75 - 0.85 W/kg | 1.92 Tesla | High-Voltage Substations & Heavy Industrial (Trnava / Nitra) |
| Conventional CRGO (M0H/M1) | 0.27 mm - 0.30 mm | 0.95 - 1.10 W/kg | 1.85 Tesla | Standard Municipal Step-Down Transformers (22kV/0.4kV) |
| Amorphous Metal Ribbon | 0.025 mm | 0.20 - 0.28 W/kg | 1.56 Tesla | Ultra-Low-Loss Rural Distribution & Renewable Power Nodes |
2. Advanced Core Assembly Techniques: Step-Lap Mitered Joint Engineering
The structural arrangement of core laminations heavily dictates hysteresis losses and acoustic noise generation. Traditional 90-degree butt joints incur significant flux distortion and localized hot spots. Our Slovak-bound transformer cores utilize automated 45-degree full-mitered step-lap geometry (1-step, 3-step, and 7-step lap patterns).
By staggering the lamination seams across multiple steps, the magnetic flux transitions smoothly parallel to the grain rolling direction. This engineering refined process yields:
- 15% to 22% Reduction in No-Load Losses: Exceeding EU Ecodesign Regulation (EU) 2019/1783 Tier 2 requirements.
- 3 dB(A) to 8 dB(A) Acoustic Noise Attenuation: Essential for indoor substations, suburban Bratislava residential zones, and hospital facilities.
- Drastic Inrush Current Suppression: Minimizing voltage dips upon grid re-energization across Slovak medium-voltage lines.
Engineering Compliance Note for Slovak Project Managers
All core laminations undergo controlled stress-relief annealing in an inert nitrogen-hydrogen atmosphere at 800°C to restore optimal magnetic domain structure after slitting and punching, guaranteeing long-term thermal stability.
Slovakia Power Grid Trends & EU Ecodesign Mandates
Understanding local distribution dynamics, industrial cluster demands, and regulatory compliance standards in Slovak Republic.
EU Ecodesign Tier 2 (EN 50708) Compliance
Slovakia enforces strict EU Ecodesign Directive limits for medium and large power transformers ($U_m \le 36\text{ kV}$). Our cores are engineered specifically to meet the maximum load loss ($A_k$) and minimum no-load loss ($C_k$) standards required for EU market deployment.
Automotive & Metallurgical Electrification
With massive automotive hubs in Bratislava, Nitra, Trnava, and Žilina, alongside steel mills in Košice, Slovakia demands transformers resistant to non-linear harmonic loads (K-Factor rated) and frequent current surges.
Renewable Energy Integration
The rapid installation of solar photovoltaic plants in Southern Slovakia and biomass generation facilities requires specialized isolation and step-up transformer cores capable of handling continuous bi-directional power flows.
Tailored Engineering for Slovak Infrastructure
Deploying specialized magnetic cores across diverse industrial, commercial, and utility environments.
A. Municipal & Substation Distribution Networks (22kV/0.4kV)
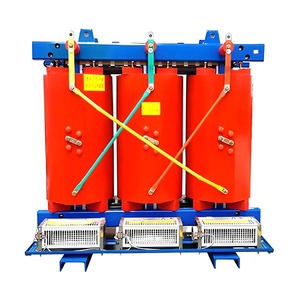
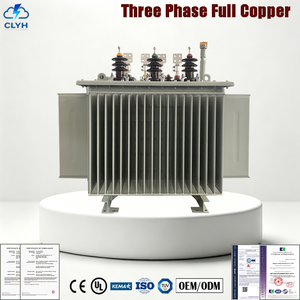
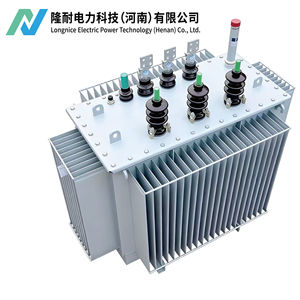
The primary distribution backbone in Slovakia relies on 22kV medium voltage feeder networks managed by regional energy companies (Západoslovenská distribučná, Stredoslovenská distribučná, Východoslovenská distribučná). Our hermetically sealed and VPI dry-type transformer cores are designed for standard oil-immersed and dry distribution units ranging from 100 kVA to 2500 kVA, delivering maximum efficiency under continuous part-load conditions.
B. Industrial Parks & Automotive Stamping Operations
Severe voltage fluctuations and harmonic distortions produced by automated robotic welding lines and heavy stamping presses in Slovak automotive manufacturing plants necessitate reinforced core clamping systems. Our heavy-duty transformer cores feature high mechanical rigidity tied with glass-epoxy banding and anti-corrosive protective coatings, preventing core migration and lamination vibration during short-circuit thermal stresses.
C. Wind Farms & Solar PV Integration Networks
Solar and wind generation sites in regions like Nitra, Trnava, and Košice require compact substations and step-up transformers with elevated ambient temperature limits. Our dry-type Cast Resin and Vacuum Pressure Impregnated (VPI) transformer cores withstand harsh thermal cycling, ensuring IP65-rated outdoor resilience and minimal no-load losses during night standby mode.
Proven Manufacturing Authority & Quality Assurance
Building trust through ISO certifications, independent laboratory type-testing, and decades of international supply experience.
ISO & International Certifications
Fully accredited under ISO 9001:2015, ISO 14001:2015, and OHSAS 18001:2007 quality management systems. Guaranteed full traceability from raw silicon steel coils to final core-coil assembly.
CPRI & ERDA Type-Tested
Our transformer designs are rigorously type-tested by renowned international laboratories including CPRI and ERDA for short-circuit withstand capability, impulse voltage endurance, and temperature rise.
State-of-the-Art In-House Testing
Equipped with automated core loss testing meters, temperature-rise test bays, partial discharge measurement equipment, and sound level chambers to verify compliance prior to dispatch.
Frequently Asked Questions by Slovak Engineers & Buyers
Direct answers to essential technical, logistics, and compliance questions for importing transformer cores into Slovakia.
Yes. All transformer core assemblies destined for Slovakia and the wider European Union are calculated and precision-cut to meet or exceed EN 50708 / Regulation (EU) 2019/1783 Tier 2 specifications for maximum allowable no-load and load losses.
We source prime-quality Cold-Rolled Grain-Oriented (CRGO) steel from leading global mills, including high-permeability domain-refined grades (0.23mm - 0.27mm, such as 23ZDH085 / M0H) as well as Amorphous metallic glass ribbon (2605SA1) for specialized high-efficiency projects.
Absolutely. We produce custom step-lap mitered cores for dry-type (VPI / Cast Resin), oil-immersed distribution transformers, arc furnace transformers, rectifier/converter duty units, and earthing transformers tailored to your specific mechanical drawings and magnetic flux requirements.
Cores are braced using high-tensile steel channels, glass-epoxy bands, and specialized tie-rods. Finished core units are packed in sea-worthy, vacuum-sealed rust-inhibiting foil within reinforced wooden crates to ensure zero core shift or corrosion during sea and land transport to Bratislava or Košice.
Each delivery includes raw material mill test certificates (MTC), magnetic loss measurement reports ($P_0$ at 1.5T and 1.7T), dimensional inspection sheets, ISO certificates, and certificate of origin documentation required for EU customs clearance.
Standard custom core manufacturing lead times range between 2 to 4 weeks depending on order volume and geometry complexity, with sea/rail transport shipping options available directly to European ports and inland logistics hubs in Slovakia.